Shotcrete nozzle blockage rarely comes from one cause alone. A damp cement pocket, oversized aggregate, or worn mixing component can interrupt flow within seconds. The signs are familiar on site: pulsing material, rising line pressure, and a nozzle operator stopping while the crew checks the hose. Small clues matter.
If you have asked, “why does a shotcrete nozzle get blocked frequently,” the answer usually involves material condition, equipment setup, or operating practice. Changes in aggregate grading and moisture can affect how the mix moves through the line. Poorly maintained air or accelerator systems may add instability. Yet symptoms can look alike, and even experienced crews can overlook a less obvious cause. Replacing a nozzle without checking the delivery path may only hide the real problem. That deserves a second look.
This guide examines ten common reasons shotcrete nozzles become blocked, including unsuitable mix consistency, foreign debris, hose bends, worn parts, and inconsistent cleaning. Each cause calls for a different check. Compare the blockage pattern with the mix design, inspect accessible components, and follow the equipment manufacturer’s operating guidance. Never treat a pressure spike as routine; stop and assess the system safely. Field conditions vary, and a checklist cannot replace competent inspection. Sometimes the cause is not obvious. Careful diagnosis can reduce downtime, limit material waste, and help crews restore a steady spray without guessing.
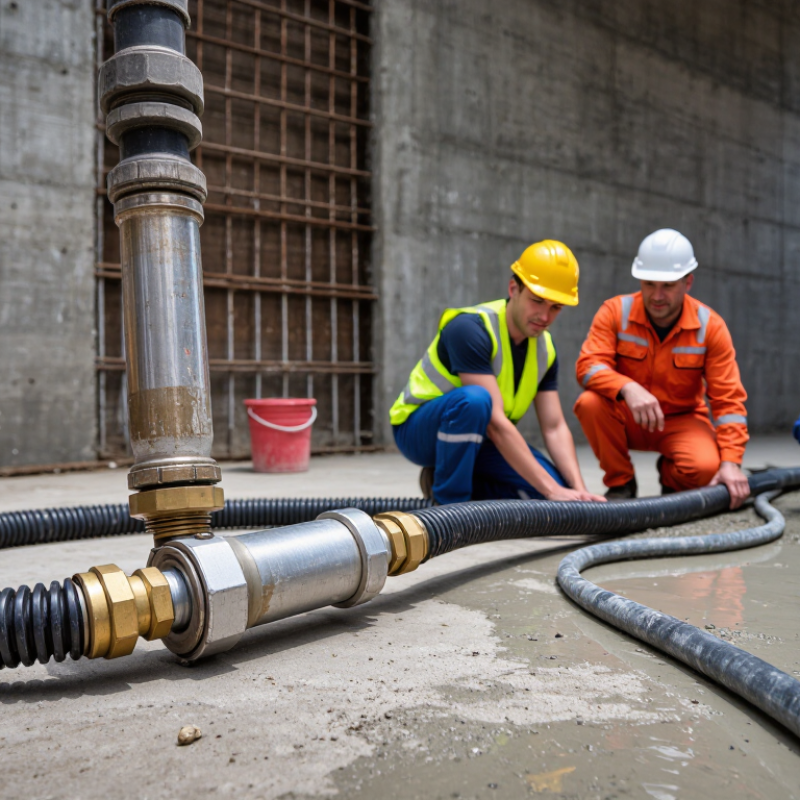
A blockage often starts as a thin layer of wet cement paste inside the nozzle. Fine particles can cling to rough surfaces, joints, or areas where the material slows. Small deposits build up. If the mix has uneven moisture, some material may feel sticky while other parts remain dry and granular. The sticky portion coats the passage; dry clumps can catch against it. Not dramatic at first.
As the opening narrows, material moves less evenly through the nozzle. Pressure can rise, and the flow may pulse instead of forming a steady stream. Each pause gives residue more time to stiffen, especially if spraying stops without clearing the line. A sudden blockage may therefore reflect several small changes, not one bad batch. It is tempting to blame only the mix, but that assumption can be wrong. Worn internal surfaces, a tight bend, or inconsistent feeding can contribute too. In practice, a brief interruption followed by a lumpy discharge is worth noting. The exact cause still needs inspection; symptoms alone rarely identify it with certainty.
Top 10 Reasons Why Shotcrete Nozzles Keep Getting Blocked
A nozzle blockage often begins in the batch, not at the nozzle. Shotcrete needs a consistent blend that can travel through the hose without separating or bridging. Aggregate grading matters: too many coarse particles, or gaps between particle sizes, can interrupt flow. Oversized stones may lodge at bends or the nozzle throat. Check the delivered aggregate against the specified grading, rather than relying on appearance alone.
Moisture changes can quietly upset the mix. Dry aggregate absorbs water; wet aggregate adds it. Either shift can make a previously reliable batch stiff, sticky, or prone to segregation. Keep moisture corrections current, and record adjustments for each load. Small steps matter. Adding water at the nozzle may seem like a quick fix, but it can weaken consistency and create rebound or placement problems. Follow the approved mix design and project requirements.
Fines and cementitious content also affect lubrication around larger particles. Too few fines may leave a harsh mix that resists pumping; excessive fines can raise water demand and make the material sticky. There is no single recipe for every aggregate source. Trial batches, sieve checks, and steady pump pressure offer better clues than guesswork. A mix can look workable in a bucket and still block under pressure. That’s easy to overlook. Review batch records alongside blockage location and frequency, then adjust only through controlled testing with qualified personnel.
Top 10 Reasons Why Shotcrete Nozzles Keep Getting Blocked
Air, Water, and Accelerator Problems That Cause Clogging
Shotcrete nozzle blockages often start with unstable air, incorrect water content, or poorly controlled accelerator dosing. Low or fluctuating air pressure may fail to move the mix evenly, leaving material to build up inside the hose and nozzle. ACI 506R-16 guidance commonly calls for about 100 psi (0.7 MPa) at the nozzle for wet-mix work, though hose length and equipment affect actual requirements. Check pressure while spraying, not only at the compressor. Wet or dirty air lines can also disrupt flow. Small details matter.
Water problems are just as costly. Too little water can make the mix stiff and difficult to pump; too much may encourage separation and unstable spraying. Either condition can leave deposits around the nozzle. Accelerator adds another variable: an incorrect setting, poor dispersion, or an unsuitable combination with the mix can trigger rapid stiffening near the outlet. Follow the mix and accelerator supplier’s technical guidance, and verify the dosing equipment before each shift. One caution: crews may blame accelerator first, while overlooking inconsistent air or water supply.
Tips: Drain air-line moisture traps, confirm water flow, and test accelerator dosing before spraying. If blockage returns, stop and inspect the hose and nozzle for hardened buildup. Record the mix, pressure, and settings; the cause is not always obvious on the first check.
Air, water, and accelerator problems that can contribute to clogging
Scores are illustrative screening estimates on a 1–10 scale, not measured incident rates. Poorly graded or damp aggregate, inconsistent air or water supply, and accelerator feed or mixing problems can all contribute to blockages. Check the mix, equipment settings, and material flow together when troubleshooting.
A blocked nozzle is not always a nozzle problem. Hose routing can restrict shotcrete flow before material reaches the nozzleman. Tight bends, sharp kinks, and long uphill runs increase resistance and encourage material to collect. Watch the hose during pumping. A section that jumps or flattens may signal a developing restriction.
Couplings matter, too. A poorly seated joint can create a small ledge where coarse aggregate catches. Worn or mismatched hose sections may also disrupt the flow path. Keep the route as direct as the site allows, support heavy hose, and check each connection before pumping. Small details count.
Equipment faults can produce similar symptoms. Inconsistent air pressure, a worn pump component, or a partly obstructed delivery line may cause pulsing instead of a steady stream. Moisture or poorly controlled material consistency can make the problem worse. It is tempting to blame the nozzle first; that diagnosis is not always right. Compare the blockage pattern with pressure changes and inspect the full line. Never open or clear a pressurized hose. Depressurize the system and follow the equipment’s operating guidance before inspection. Sometimes the cause is less obvious than expected.
| No. | Potential Cause | How It Disrupts Delivery | What to Check | Practical Corrective Action |
|---|---|---|---|---|
| 1 | Sharp bends or kinks in the delivery hose | A tight bend restricts the passage and can cause material to accumulate, increasing the chance of a plug. | Inspect the full hose run, especially at the pump outlet, couplings, and around corners. | Reroute the hose with gradual curves and keep it within the hose manufacturer’s minimum bend radius. |
| 2 | Excessive hose length or unnecessary fittings | Long runs and multiple couplings or reducers increase flow resistance and create places where material can collect. | Review hose length, internal diameter, reducers, and the number of connections against the equipment setup requirements. | Use the shortest practical hose route and compatible fittings; avoid abrupt changes in hose diameter. |
| 3 | Hose sagging, loops, or poor support | Low spots and loops can encourage material to settle or move unevenly, particularly during interruptions in pumping. | Look for unsupported sections, sharp vertical changes, and areas where the hose forms a pocket. | Support and position the hose to maintain a smooth, direct route. Follow the approved setup for the mix and equipment. |
| 4 | Aggregate grading or maximum particle size out of specification | Oversized particles or an unsuitable grading can bridge at restrictions, couplings, or the nozzle passage. | Check the approved mix design, aggregate grading, and particle size against the pump, hose, and nozzle requirements. | Use correctly graded aggregate and keep the mix within the specified maximum particle size for the delivery system. |
| 5 | Inconsistent moisture or mix workability | A mix that is too dry, too stiff, or inconsistent may not move uniformly through the hose and can build up in the nozzle. | Check batching records, aggregate moisture, water addition, and whether the mix is consistent from load to load. | Correct batching and moisture control in accordance with the approved mix design; do not add water at the nozzle as an improvised fix. |
| 6 | Hardened material or residue left in the hose or nozzle | Residual concrete narrows the flow passage and provides a surface for fresh material to catch and accumulate. | Inspect the nozzle, hose ends, and couplings for hardened deposits, damaged liners, or restricted openings. | Clean the system promptly using the equipment’s approved procedure, and replace components that remain restricted or damaged. |
| 7 | Worn, damaged, or mismatched hose and couplings | A damaged liner, poorly aligned connection, or incompatible fitting can create an internal obstruction or disrupt material flow. | Check for bulges, exposed reinforcement, liner damage, coupling misalignment, and signs of leakage. | Replace defective parts with components rated and sized for the application; secure connections according to the manufacturer’s instructions. |
| 8 | Insufficient or unstable conveying air (pneumatic systems) | In dry-mix or air-assisted delivery, inadequate or fluctuating air supply can reduce conveying performance and contribute to material buildup. | Check air pressure and flow at the relevant operating point, along with leaks, blocked filters, and undersized air lines. | Restore the specified air supply and repair leaks or restrictions; verify compressor capacity under actual operating conditions. |
| 9 | Uneven pump feed or worn pumping components | Pulsing or interrupted material flow can make delivery less uniform and increase the likelihood of buildup in the line or nozzle. | Review pump operation, material feed, wear parts, pressure behavior, and any repeated interruptions or unusual pulsation. | Service the pump as specified, replace worn components, and maintain a steady feed within the machine’s operating limits. |
| 10 | Accelerator buildup or incorrect dosing (where used) | Deposits in the accelerator line or nozzle, or an unsuitable dosing setup, can interfere with the nozzle passage and material flow. | Inspect the dosing line and injection point; verify the product instructions, metering equipment, and cleaning routine. | Follow the approved accelerator dosage and cleaning procedure, and keep the injection system clear and correctly calibrated. |
Safety note: Stop and depressurize the delivery system according to the equipment procedure before inspecting or clearing a blockage. Never open a pressurized hose or nozzle.
Repeated nozzle blockages often start before spraying. A mix that waits in the hose can lose workability, while a poorly flushed reducer traps paste and coarse particles. ACI 506R-16 identifies consistent material delivery and suitable equipment operation as key shotcrete controls.
In practice, watch the mix at the hopper: dry pockets, uneven feed, or a pulsing hose deserve attention.
Small clues matter.
Cleaning habits can turn one delay into a recurring problem. Clear the line promptly between batches, following the equipment maker’s procedure; do not leave wet material to stiffen around bends or couplings. Check reducer throats and hose joints for hardened rings, then replace worn or damaged sections.
ASTM C94/C94M gives ready-mixed concrete a common discharge limit of 90 minutes or 300 drum revolutions, whichever comes first, unless otherwise specified. That is not a shotcrete hose-time allowance. Still, it shows why elapsed time and agitation matter.
A rushed cleanup may look adequate. It often isn’t. After clearing a blockage, record where it formed and what the mix looked like; crews sometimes repeat the same mistake because nobody writes it down.
Unstable air pressure, incorrect water content, accelerator dosing, and restricted hose routing can all contribute. The nozzle may not be the source.
Guidance commonly calls for about 100 psi (0.7 MPa) at the nozzle. Hose length and equipment affect actual needs, so check pressure while spraying.
Too little water can make the mix stiff and hard to pump. Too much may encourage separation and unstable spraying. Neither helps.
Verify the dosing equipment and follow the mix and accelerator supplier’s technical guidance. Poor dispersion or incorrect settings can cause rapid stiffening near the outlet.
Tight bends, sharp kinks, and long uphill runs can increase resistance. Watch for hose sections that jump or flatten.
Yes. A poorly seated joint can leave a ledge where coarse aggregate catches. Check connections before pumping.
Compare blockage patterns with pressure changes, then inspect the hose and nozzle for hardened buildup. Record the mix, pressure, and settings. The cause may still be unclear.
Depressurize the system and follow the equipment’s operating guidance before inspection. Never open or clear a pressurized hose. Safety is easy to overlook.
Shotcrete nozzle blockages usually develop when material flow becomes uneven, allowing wet mix or partially hydrated cement to collect inside the nozzle and restrict its passage. Understanding why does a shotcrete nozzle get blocked frequently starts with the mix itself: poorly graded or oversized aggregate, excessive fines, inconsistent moisture, and unsuitable mix proportions can all make concrete harder to convey. Inadequate or fluctuating air pressure, incorrect water delivery, and accelerator feed problems may further disturb the flow and encourage material to build up.
Delivery equipment and work practices also matter. A hose with sharp bends, excessive length, or internal wear can increase resistance, while loose connections or pressure problems may interrupt a steady stream. Repeated blockages can also result from starting and stopping abruptly, operating outside recommended settings, or failing to clean the nozzle and hose promptly after use. Consistent mix checks, stable air and water supply, sensible hose routing, careful operation, and thorough cleaning help reduce interruptions and maintain reliable shotcrete delivery.
SSG Machinery